
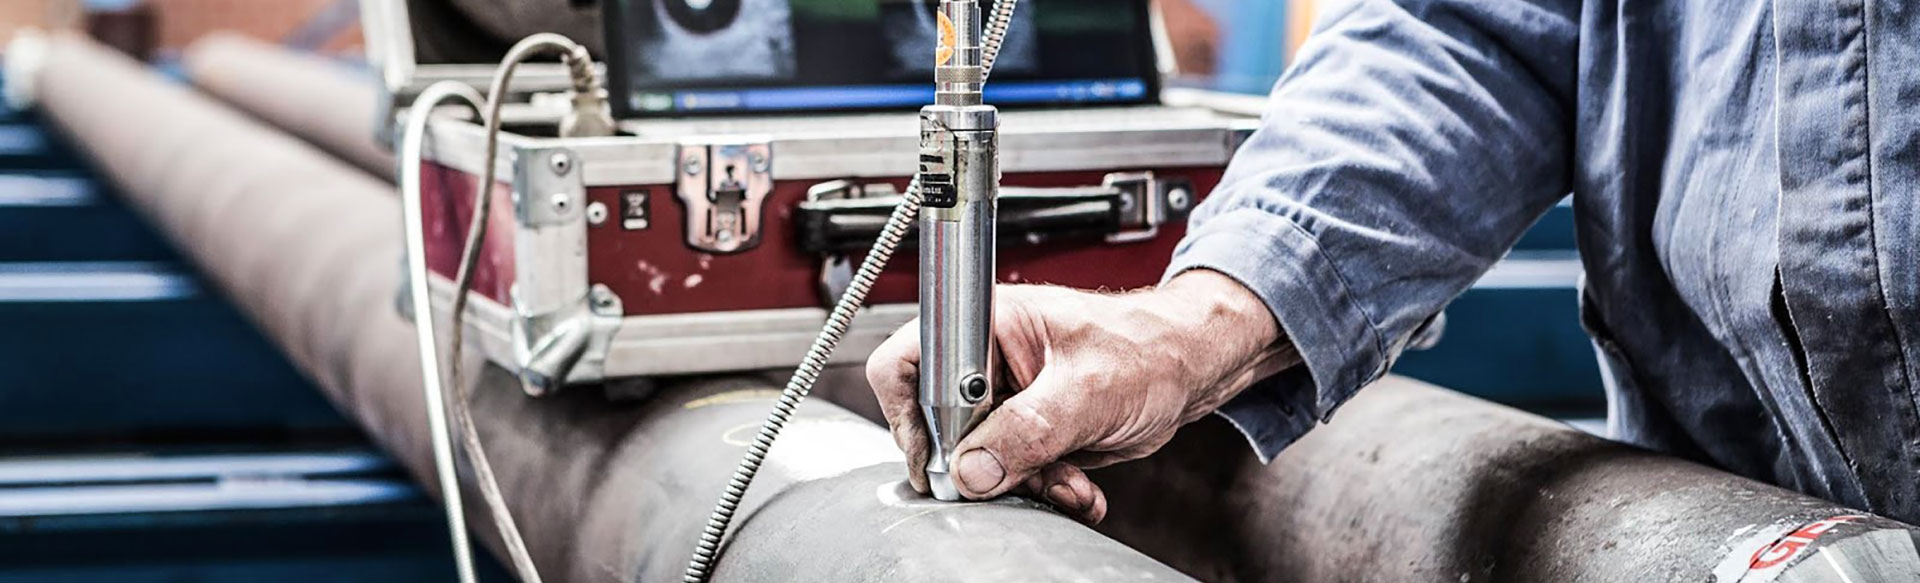
The phased array technique was initially developed for Swedish nuclear power plant operators to meet the need to analyze stainless steel pipes up to 76 mm in diameter. Phased array testing is a type of ultrasonic testing in which a group of sound waves is introduced into the sample. EUROLAB, specializes in developing phased array testing methods using the latest robotic technologies.

Your benefits from progressive sequence testing
About the Progressive Sequence Test
Phased array testing, EUROLAB The phased array device is capable of detecting and imaging inhomogeneities very precisely, while analyzing bundles of sound pulses and their behavior within a test sample.
Our latest mechanized staged array solutions are able to document error indications quickly and efficiently, so progressive array inspection is particularly useful in alleviating the burden of time-critical plant shutdowns where X-ray windows are often relatively short.
EUROLAB We have been optimizing our phased array methods and technologies for years and continually train our experienced ultrasonic inspectors in the rapidly growing field of phased array inspection to deliver the reliability and safety our customers demand.
Distorted errors defined by the orientation of the responses with respect to the general resource geometry and structural noise. This is evident in both direct and modal transformed responses. Inspection includes detection, characterization, length and height sizing of environmental defects in the source and heat affected zone (HAZ).
Our mechanized staged sequence testing solutions include:
EUROLAB, with its highly expert team and internationally accredited laboratories, Progressive Sequence Tests It performs all test, analysis, measurement, evaluation and report generation services completely and reliably.
To get an appointment, to get more detailed information or to request an evaluation, you can ask us to fill in our form and reach you.

