

The standard “DIN 53295 Testing of sandwich structures - Peel test with drum aid”, published by the German Institute for Standardization (DIN), describes a test method for determining the peel resistance (or peel strength) of adhesive bonds in sandwich structures. Sandwich structures typically consist of two thin, rigid surface layers (e.g., aluminum or composite layers) bonded to a lightweight core material (e.g., honeycomb, foam, or balsa wood). These materials are widely used in aerospace, automotive, railway vehicles, building panels, and other industries where high strength-to-weight ratios are required.
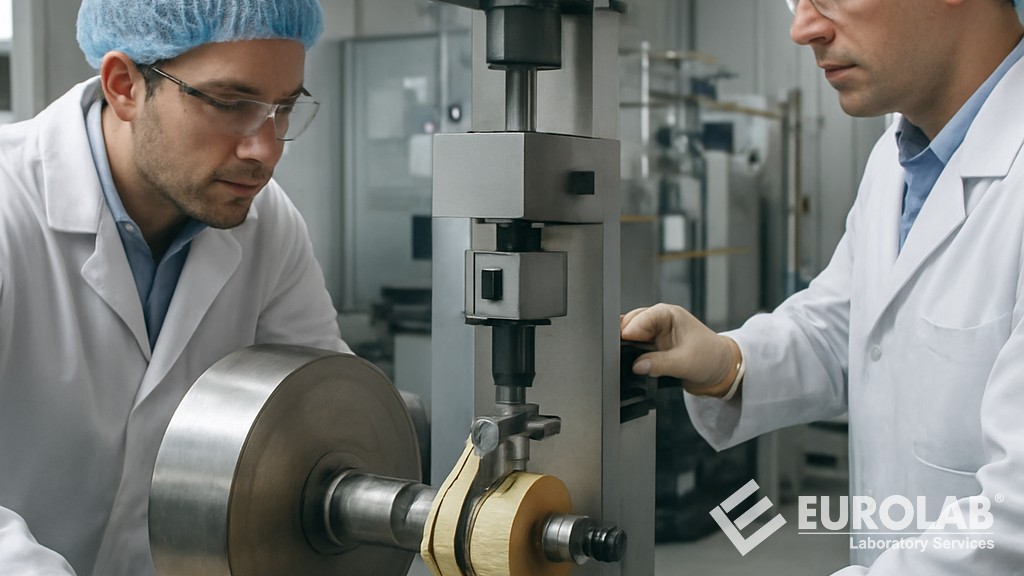
This standard focuses on evaluating how well the adhesive holds the surface layer to the core under peeling forces. Poor adhesion can lead to delamination, a critical failure mode in sandwich panels. The test provides a quantitative measure of bond quality, typically expressed as peel moment (torque per unit width) or average peel force.
This method uses a special fixture known as a climbing drum (or drum peeling apparatus). The working principle of the test is as follows:
The DIN 53295 standard is closely related to, and often cited alongside, other international standards for the same or similar climbing drum peeling test:
Many modern test setups are designed to comply with all three standards simultaneously.
The DIN 53295 standard continues to be actively referenced in recent years in test equipment specifications, research papers (e.g., on aluminum foam cores or reinforced fabricated truss sandwiches), and industrial applications.
In short, the DIN 53295 standard is based on measuring the force required to peel the coating layer from the core at a specific angle and speed.
A sandwich structure typically consists of three layers:
This structure provides the advantage of high rigidity/low weight in aerospace, automotive, construction, and marine applications.
The DIN 53295 standard is used to evaluate the following characteristics:
It is particularly important in quality control and research and development activities.
The testing process essentially follows these steps:
The result is usually expressed as: Peel strength = Force / Sample width.
The standard typically specifies the following sample characteristics:
The following information is reported after the test:
The type of fracture is critical in determining whether it is due to a manufacturing defect or a material weakness.
The DIN 53295 standard is used particularly in the following areas:
The DIN 53295 standard is considered important for the following reasons:
For many years, our organization, with its competent and experienced staff, has been understanding the needs of its clients, providing the advanced testing services they require, and assisting them in the establishment, implementation, and improvement of management systems. Within this framework, we also provide testing services in accordance with the DIN 53295 standard.
To get an appointment, to get more detailed information or to request an evaluation, you can ask us to fill in our form and reach you.

