

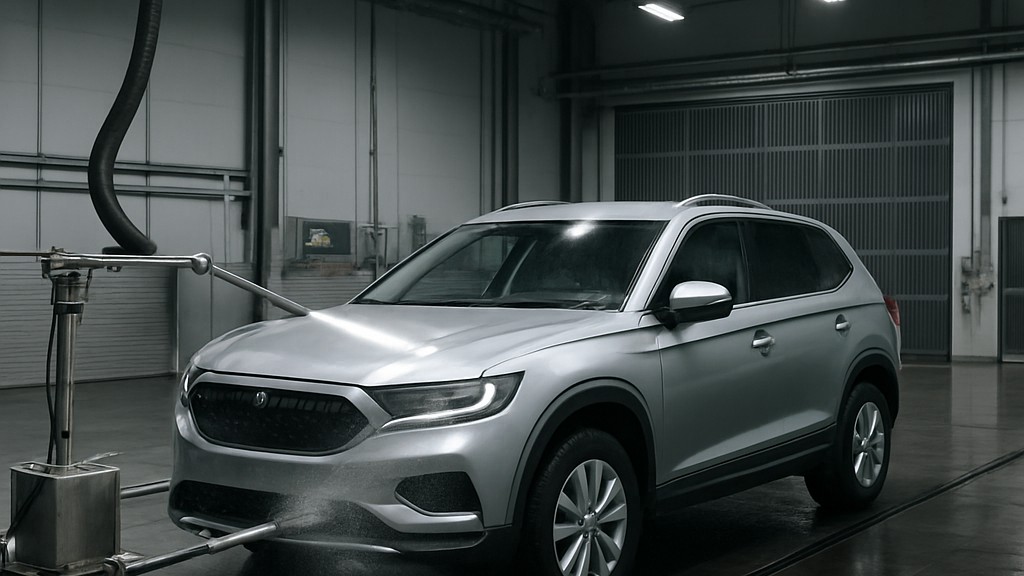
The standard "DIN EN ISO 16925 Paints and varnishes - Determination of resistance of coatings to pressurized water jets," developed by the German Institute for Standardization (DIN) and subsequently published by the International Organization for Standardization (ISO), describes a test method for assessing the resistance of coatings to pressurized water jets. This test method simulates the effects of a pressurized water jet on a coating. While primarily used in the testing of automotive coatings, this method has also been applied in other areas.
For the purposes of this standard, the following definitions apply in addition to the terms and definitions given in ISO 4618:
In principle, the resistance of a coated test specimen to loss of adhesion strength is tested with a water jet of a defined pressure. The extent of damage to the test specimen depends primarily on the adhesion strength, as well as the gap between the nozzle and the test piece, volumetric flow rate, test duration, nozzle geometry, impact area, impact angle, jet water temperature, and the cutting and scoring tool. Assessment is performed by visually comparing images where characteristic values correlate with the peeled areas. The separation line (plane) of peel should be specified in the test report (e.g., substrate/primer layer).
In these tests, a pressurized water jet consisting of a high-pressure pump and nozzle is used. The high-pressure pump delivers water from a storage tank. To prevent effects caused by pressure fluctuations, the pressure and volumetric flow rate at the nozzle, described below, must be adjustable. The water temperature must be adjustable to plus or minus 2 degrees Celsius. The temperature must be adjusted in accordance with Annex A. The pressure side of the unit must be equipped with the necessary safety devices, such as a pressure relief valve and a bypass valve. If the spray is irregular, a flow-settling section can be installed before the nozzle. Vibration of the water jet at the pump nozzle is unacceptable. To achieve reproducible results, the nozzle must be mechanically secured, and the test specimen must be secured against slipping. To adjust the volumetric flow rate, a nozzle with a 25-degree jet angle and a volumetric flow rate of 6 l/min at 2 MPa (20 bar) is required. Furthermore, the technical data specified in the standard, such as volumetric flow rate, pressure, temperature, and spray duration, must be available. The schematic structure of a pressurized water jet device specifically constructed for these tests is shown in the figure included in the standard.
The tests also use a cutting or scribing tool and a time measuring device (stopwatch) to be agreed upon by the parties involved.
A representative sample of the product to be tested is taken according to ISO 15528. Each sample is examined and prepared for testing according to ISO 1513. Test specimens should preferably be flat. The size of the test specimens and the number of tests should be agreed upon by the relevant parties. Test specimens (building components) may have varying adhesion strengths. It is recommended to test different sections of the test specimen (building components).
The coating, drying/curing, and baking conditions must be determined. Before testing, coated test specimens should be conditioned at 60°C for 48 hours or at room temperature for 7 days. After conditioning at 60°C, the specimen should be cooled to room temperature before cutting or scoring. Determine the dry film thickness of the coating in microns according to one of the procedures specified in ISO 2808.
When placing the cut or scribe, it is essential to ensure that the test specimen is securely fastened. Using a cutting or scribe tool, both cuts or scribes are placed vertically through the coating into the substrate. The depth of the cut or scribe to the substrate should be as small as possible. If the geometry of the part allows, the first cut or scribe should be at least 100 mm long. A second cut or scribe, at least 20 mm long, is placed at an angle. The cuts or scribes should be placed in a straight line at an angle of approximately 30 degrees. An automatic cutting or scribe device can be used. Coating residue should be removed from the cut or scribe area. The depth of the cut or scribe to the substrate affects the results. Cutting or scribe tools should be checked regularly and replaced if necessary.
After placing the test sample in the device (e.g., using a spacer block), the gap between the test sample and the nozzle is calibrated. The pressurized water jet device is operated at room temperature.
Three test methods and three possible scribing instruments are preferred. Agreement must be reached on the test method to be applied, the scribing or cutting instrument to be used, and the water pressure.
The parameters for the three test methods are listed in the table provided in the standard, based on water temperature, impact angle, nozzle-to-sample gap, flow rate, and spray duration. Deionized water must be used for spraying. When using automatic and manual devices, the test sample is fixed to the water jet. The jet strikes the longer of the two dashes or lines, centered above the intersection point.
Regardless of which coating is damaged, damage is detected by loosening or peeling of the coating. The assessment is performed visually and compared with the sample drawings. During the visual assessment, a characteristic value between 1 and 5 is obtained, depending on the degree of damage, by comparison with the drawings. A characteristic value of 0 corresponds to no damage. In addition to the assessment, it should be noted whether any separation is caused by the main separation level or the film in question. The results of the visual assessment are reported, depending on the method used. Additionally, overall damage can be assessed by measuring the areas of flaking (maximum width in millimeters or area in square millimeters). Overall damage is calculated by summing all damaged areas on the test sample. Even the smallest areas of flaking are measured and calculated, and all areas are added to the overall damage.
This standard replaces the standard “DIN 55662 Paints and varnishes - Coatings for the automotive industry - Testing of resistance to pressurized water jet”.
Our organization, which has been supporting businesses across all sectors for years through a wide range of testing, measurement, analysis, and evaluation activities, has a strong team of employees who closely follow global developments in science and technology and are constantly improving themselves. In this context, we also provide testing services in accordance with the DIN EN ISO 16925 Paints and varnishes - Determination of the resistance of coatings to pressurized water jets.
To get an appointment, to get more detailed information or to request an evaluation, you can ask us to fill in our form and reach you.

