

The standard “MAN M 3150-2 Surface quality – Assessment of the final coating – Truck”, developed by the automotive company MAN, describes a procedure for assessing the final coating of trucks in terms of surface quality.
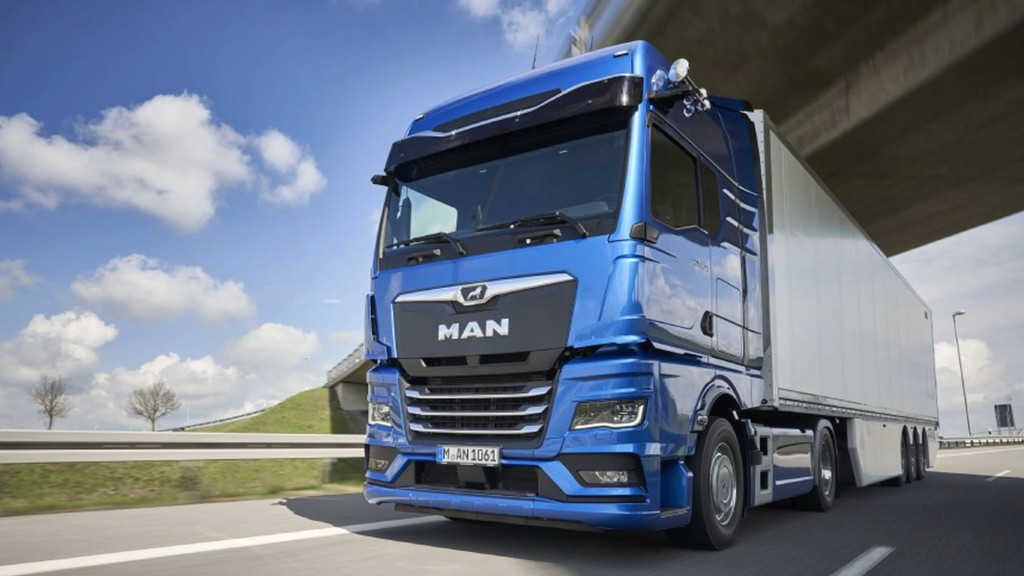
Essentially, the MAN M 3150 series of standards includes requirements for the uniform assessment of the surface quality of cavities, coatings as well as the structure and colour matching on MAN commercial vehicles (cabin, cabin add-on parts and chassis). In short, this series of standards is designed to allow the uniform assessment of the surface quality and the structure and colour matching of coatings on MAN commercial vehicles. In general, this standard applies to trucks. Special regulations may apply for military vehicles.
This series of standards applies to both in-house parts and purchased parts, regardless of the quality and type of component material.
The purpose of the MAN M 3150-2 standard is to determine uniform criteria for the assessment of the surface quality of the final coating in order to guarantee a uniform surface condition for trucks in terms of colour, gloss and structure. These requirements are derived from customer requirements and state-of-the-art technology. The standard distinguishes between painted surfaces and textured painted and grained surfaces.
The required surface quality must be within the tolerance ranges required for surface structure, gloss level and colour for trucks. The measured values specified in the second part of the MAN M 3150-2 standard apply only to the cab and cab attachments (this includes the bumper, the mudguard behind the front axle and the side panels). The requirements regarding failure patterns specified in the third part apply to the chassis and chassis attachments.
The requirements for the substrate coating (structure, colour) are specified in the technical delivery conditions of the coating materials (standards M 3094, M 3031, M 3022 etc.). In particular, it must be ensured that the filler colour of the cabin is the same as that of all additional parts.
The test of the degree of gloss should be carried out according to the relevant upper layer standards (M 3094, M 3031, M 3022 standards). In the normal case, high gloss, reflectometer range according to DIN EN ISO 2813 standard, 20 degree incidence angle and at least 80 unit gloss are required.
Colour and gloss level testing should generally be carried out in accordance with the specified coating standard (e.g. M 3018, M 3300, M 3022, M 3031, M 3094 standards). Special regulations should be taken into account for special vehicles. For high gloss, a maximum of 1 percent difference in gloss level is allowed for components in Zone 2 and Zone 10 surfaces. For matt surfaces, design or military-specific tolerances apply.
This standard defines the evaluation criteria for the evaluation of color deviations and the measurement and evaluation conditions for the instrument-based determination of color differences in the top coat paint coating of cabinets and cabinet connections. The evaluation of painted connection parts with a grained coating is defined in the M 3150-7 standard.
For the purposes of this standard,
Among the numerous tests, measurements, analyses and evaluations carried out for businesses in various sectors, our organization also provides testing services defined in the “MAN M 3150-2 Surface quality - Evaluation of final coating - Truck” standard with its trained and expert staff and advanced technological equipment.
To get an appointment, to get more detailed information or to request an evaluation, you can ask us to fill in our form and reach you.

