

The standard “MAN M 3150-6 Surface quality - Assessment of the final coating - Buses”, developed by the automotive company MAN, describes a procedure for assessing the final coating within the scope of surface quality of buses.
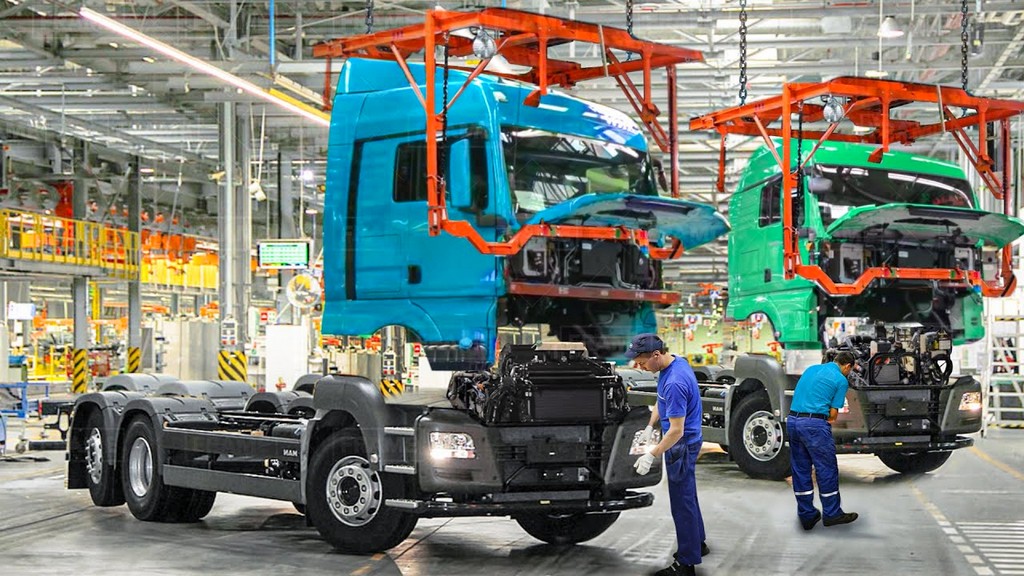
Essentially, the MAN M 3150 series of standards was designed to allow the surface quality and the structure and colour harmony of coatings on MAN commercial vehicles (cabin, cabin add-on parts, chassis and bus exterior coating) to be assessed uniformly. The MAN M 3600 standard is also fully valid in this regard.
This series of standards applies to both in-house parts and purchased parts, regardless of the quality and type of component material (sheet metal, plastic).
The purpose of this part of the M 3150 series of standards is to determine uniform criteria for the assessment of the surface quality of the final coating in order to guarantee a uniform surface condition in terms of colour, gloss and structure on buses. The requirements are derived from customer requirements and state-of-the-art technology. The MAN M 3150-6 standard distinguishes between painted surfaces and textured painted and grained surfaces. Parts 2 and 3 apply to painted surfaces, while Parts 4 and 5 apply to textured painted or grained surfaces.
The required surface quality is within the required tolerance ranges for surface structure, gloss level, turbidity and color for buses. In this regard, the requirements in accordance with the table given in the standard are taken into account.
The requirements for the substrate coating (structure, colour) are specified in the technical delivery conditions of the coating materials (M 3094, M 3031, M 3022 and similar standards). The MAN M 3150-5 standard applies to the primer coating.
The test of the degree of gloss should be carried out in accordance with the relevant upper layer standards (M 3094, M 3031, M 3022 standards). In the normal case, the high gloss should be in accordance with the reflectometer range defined in the DIN EN ISO 2813 standard, the angle of incidence should be 20 degrees and the power should be at least 80 units.
Colour and gloss level testing should generally be carried out in accordance with the specified coating standard (e.g. standards M 3018, M 3300, M 3022, M 3031, M 3094). Special regulations must be observed for special vehicles. For high gloss surfaces, the following applies: A maximum of 10 percent difference in gloss level is permitted for Zone A and Zone B surfaces when comparing components with each other.
Colorimetric evaluation tests complying with this section are performed if the relevant test equipment requirements are met.
The MAN M 3150-6 standard defines the evaluation criteria for the assessment of color deviations including bus paint and inserts, as well as the measurement and evaluation conditions for the determination of apparatus-based color differences. The assessment of painted and colored inserts with a grained surface is defined in the M 3150-7 standard.
For the purposes of this standard,
An important prerequisite for visual assessment is that observers with good colour discrimination must be used for colour matching (DIN 6173).
Among the numerous tests, measurements, analyses and evaluations carried out for businesses in various sectors, our organization also provides testing services defined in the “MAN M 3150-6 Surface quality - Evaluation of final coating - Bus” standard with its trained and expert staff and advanced technological equipment.
To get an appointment, to get more detailed information or to request an evaluation, you can ask us to fill in our form and reach you.

